Sulfuric acid dilution equipment is designed for controlled industrial preparation of diluted sulfuric acid. System selection should consider acid concentration, required output, materials of construction, heat management, automation and project-specific safety requirements.
Sulfuric acid dilution equipment is used in industrial applications where concentrated sulfuric acid must be diluted to a required process concentration. Because the dilution reaction releases significant heat, equipment design should focus on controlled dosing, heat management, corrosion resistance, process monitoring and operator protection.
The appropriate sulfuric acid dilution system should be selected according to the acid concentration, required output, operating schedule, downstream process and site safety requirements.
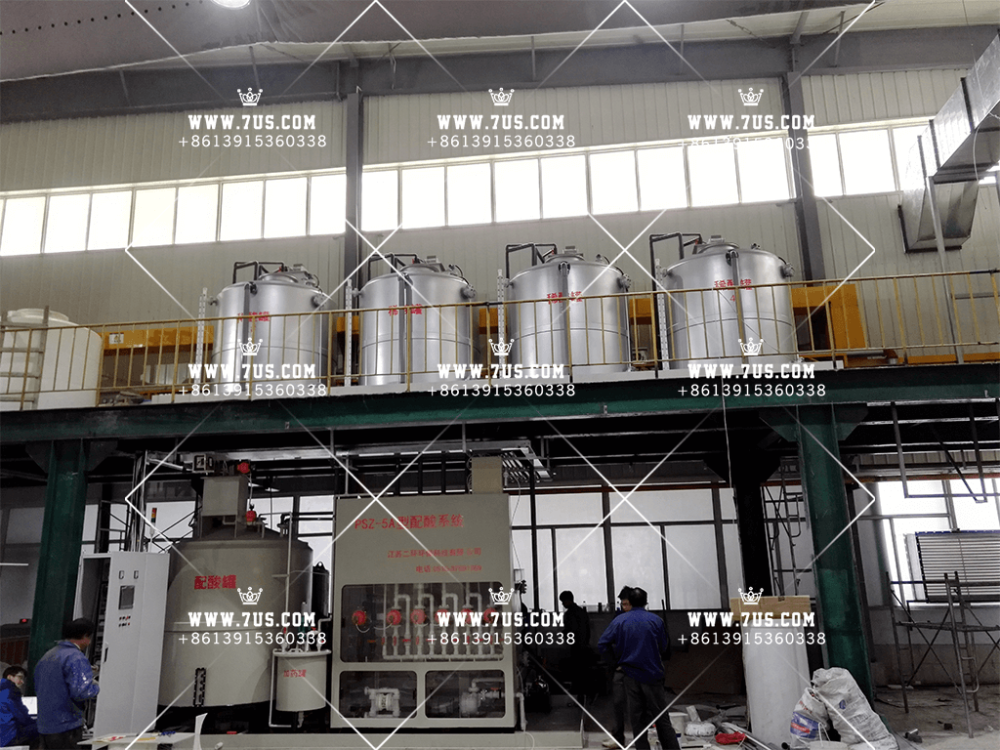
Manual handling of concentrated sulfuric acid can create operational and safety risks. Industrial dilution equipment provides a more controlled process by integrating chemical-resistant tanks, metering devices, mixing arrangements, heat-management components and monitoring instruments.
A properly designed system can help improve concentration consistency, reduce manual handling and support more reliable operation in industrial processes.
1. Materials of construction: Tanks, pipelines, valves, pumps and instruments should use materials suitable for the sulfuric acid concentration, temperature and process conditions.
2. Heat management: The system should be designed to manage the heat released during dilution. Depending on the project, this may include controlled feed arrangements, mixing design, cooling capacity and temperature monitoring.
3. Process control: Metering, level monitoring, temperature monitoring and interlocks can help maintain stable operation and reduce the risk of incorrect dosing.
4. Containment and maintenance: The equipment layout should provide suitable containment, drainage, inspection access and maintenance space. The design should also consider safe replacement of consumable parts and instruments.
Sulfuric acid dilution systems should be designed and operated by trained personnel under site-specific procedures. Required personal protective equipment, ventilation, emergency response provisions and any applicable local requirements should be determined for the actual installation.
Equipment selection should be based on the complete process conditions rather than concentration alone. Provide the acid concentration, target concentration, required output, operating temperature and installation requirements when requesting a technical proposal.
7US supplies industrial sulfuric acid dilution equipment for project-specific applications.
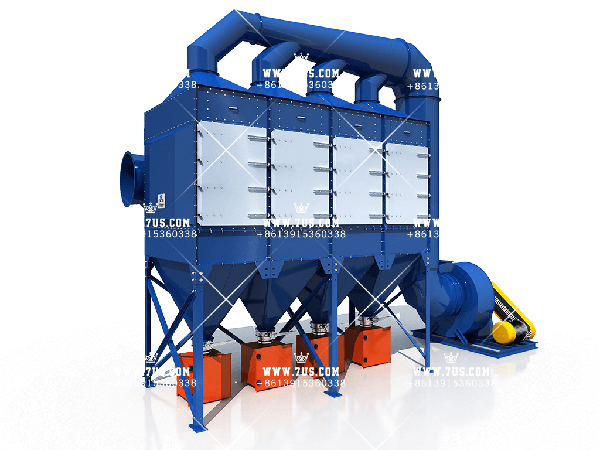
1. Vertical modular cartridge dust collector designed for high dust loading, fine dry dust and large-airflow industrial filtration applications. 2. Standardized DHC filtration modules can be combined to increase total airflow, allowing flexible system expansion according to project requirements. 3. Vertical cartridge arrangement with side-door access and eccentric cam fixing allows convenient filter inspection and replacement. 4. Single-stage cartridge filtration, two-stage cartridge + HEPA filtration, and three-stage cartridge + HEPA + activated carbon filtration configurations are available. 5. HEPA final filtration can be added for applications requiring very low particulate emissions, while activated carbon can be used as an additional polishing stage for suitable odor or VOC applications. 6. Standard single-module airflow ranges from 4,000 to 10,000 m³/h, and multiple DHC8 modules can be combined for systems up to 80,000 m³/h as shown on this page. 7. Equipment dimensions, filter media, color and OEM configuration can be customized according to project requirements.
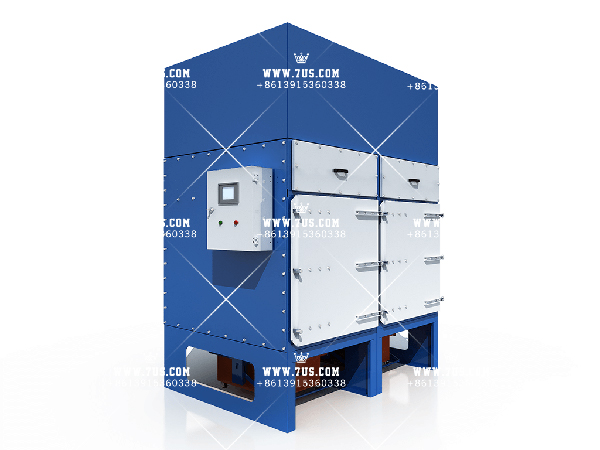
1. Vertical all-in-one cartridge dust collector designed for compact installation, convenient operation and efficient dry dust filtration. 2. Suitable for compatible dry dust and fume applications with dust-laden air temperatures below 120°C. 3. Vertical cartridge arrangement with side-door access allows convenient cartridge inspection and replacement. 4. Pleated cartridge filters provide a large filtration area within a compact equipment footprint, with automatic pulse-jet cleaning for routine filter cleaning. 5. Optional HEPA final filtration and activated carbon filtration can be added according to the required particulate and odor/VOC treatment needs. 6. DHC-YT series models are available with airflow capacities from 4,000 to 12,000 m³/h. 7. Equipment color, filter media, voltage, frequency and OEM configuration can be customized according to project requirements.
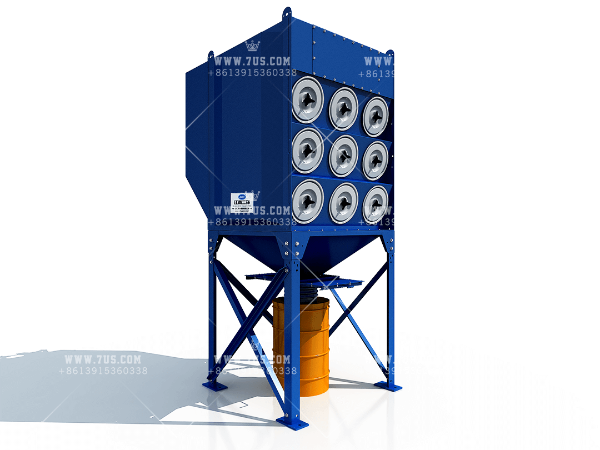
1. Downflow oblique modular cartridge dust collector designed for flexible capacity expansion through standardized modular units. 2. Compact modular construction helps reduce installation footprint and allows the equipment to be divided into transport-friendly sections for easier shipping and assembly. 3. Pleated cartridge filters provide a large filtration area within a compact equipment volume, with automatic pulse-jet cleaning for routine filter cleaning. 4. Standard EHDFT modules can be combined to increase total airflow according to project requirements, with configurations available up to 100,000 m³/h. 5. Optional two-stage filtration with cartridge filters and HEPA final filtration is available for applications requiring additional filtration performance. 6. Stainless steel construction, abrasion-resistant inlet arrangements, exhaust dampers and explosion protection components can be evaluated according to the application. 7. Suitable for compatible dry dust and fume applications without oil or water, subject to the confirmed dust characteristics and project safety requirements. 8. Equipment configuration, filter media, color a
No. 173, Wuwei Industrial Zone, Xushe Town, Yixing, Jiangsu, China© 1994-2026 7US.com. All rights reserved | Privacy PolicySite map
Phone